In the modern agricultural supply chain, cultivating high-quality produce at the farm is merely the beginning. The greatest challenge lies in logistics how to preserve the flavor, color, and nutritional content of fruits and vegetables during long transit periods.
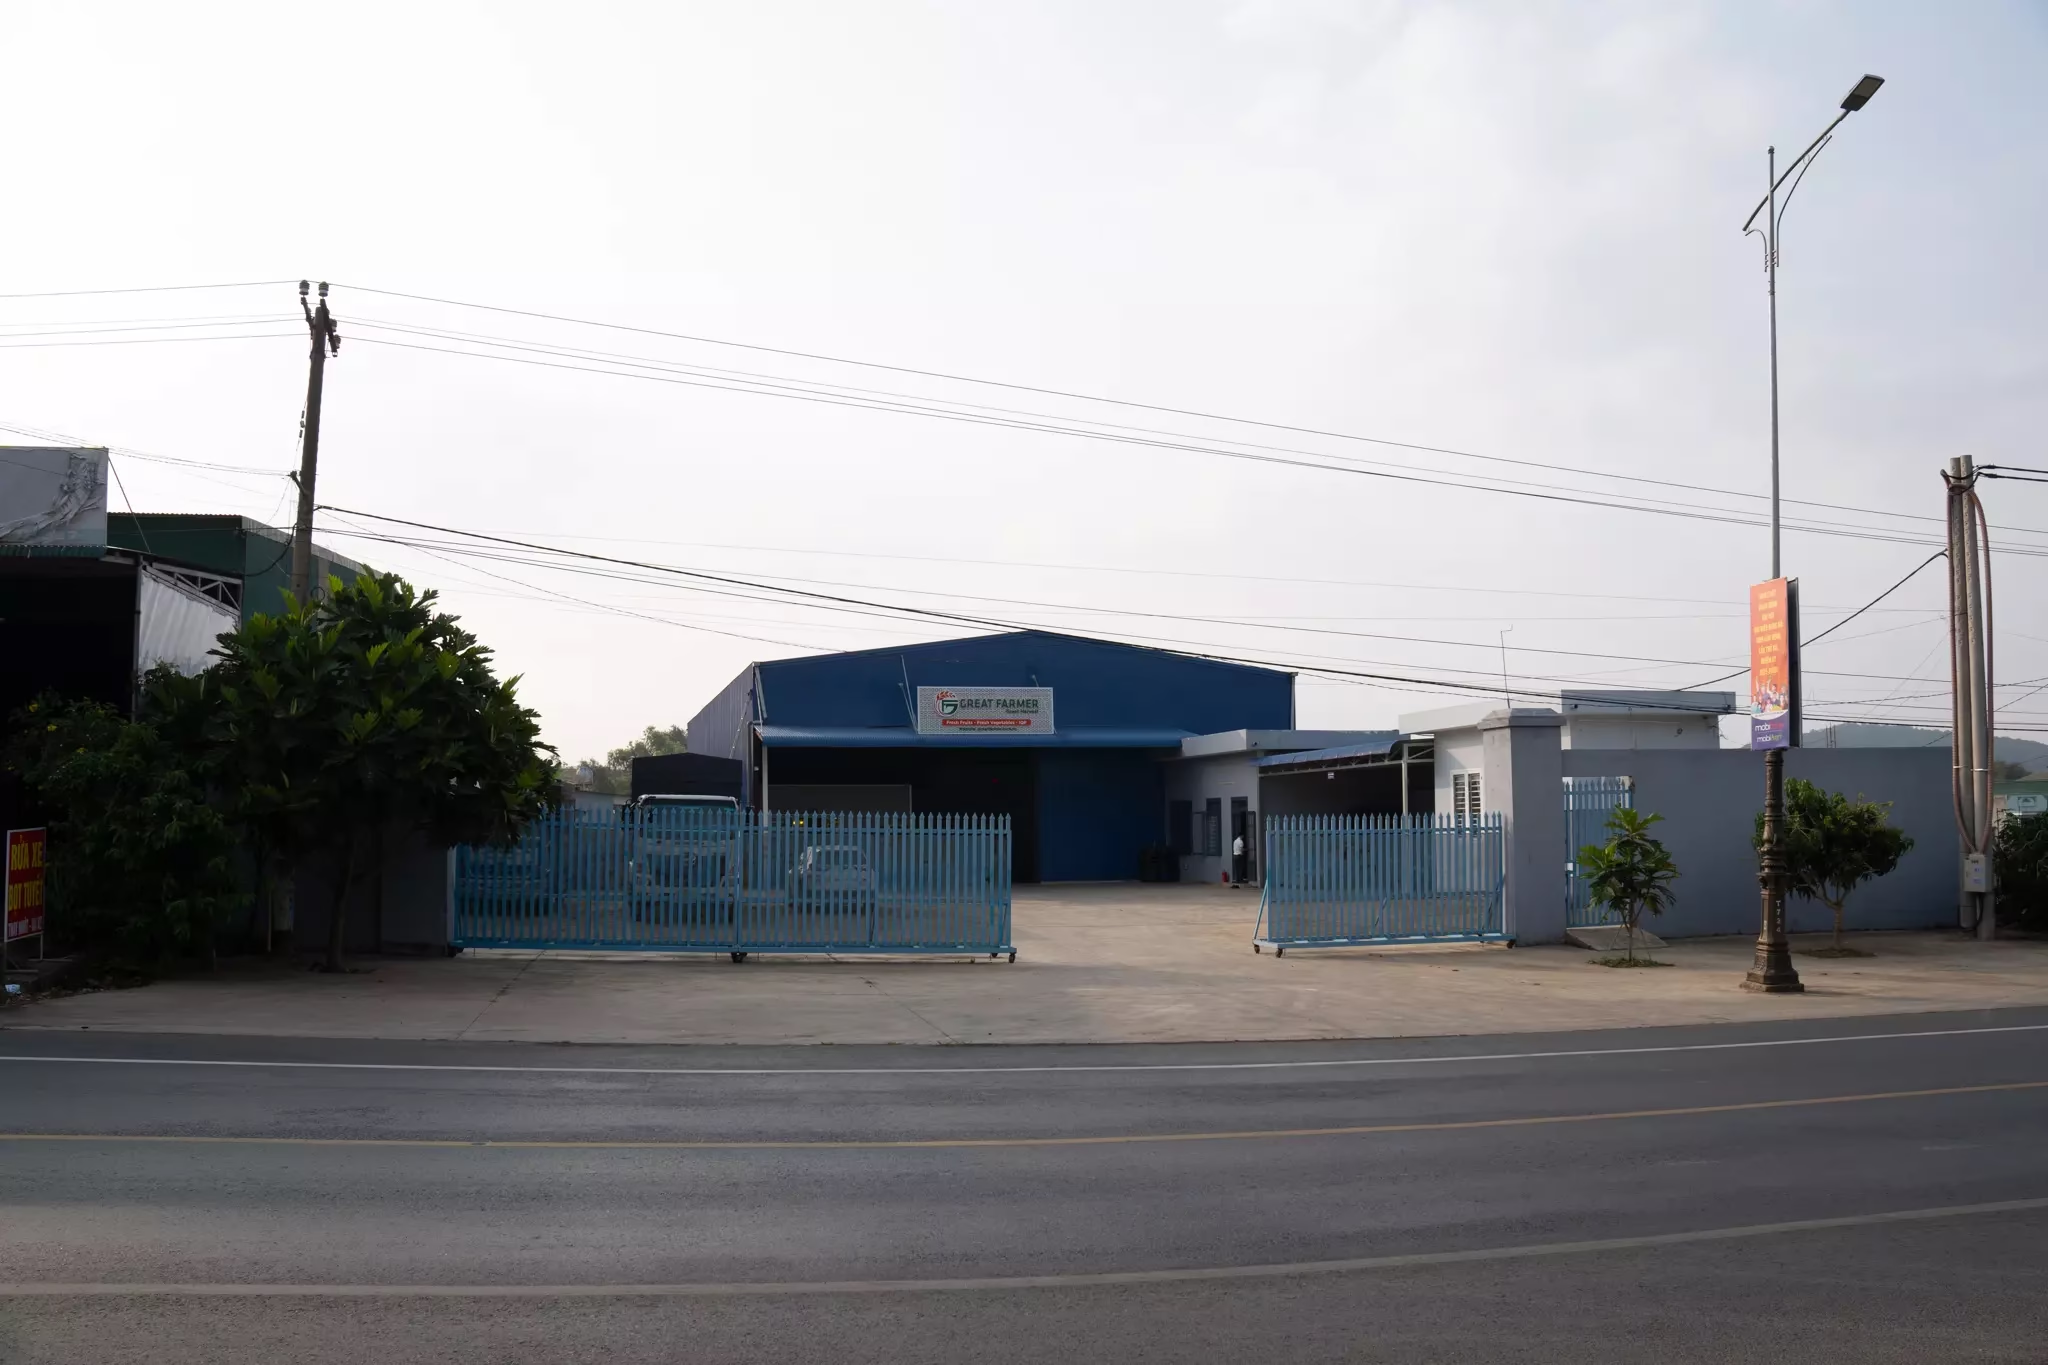
The answer lies in post-harvest handling capabilities. At Great Farmer, we understand that investing in a processing and packaging plant and a standard agricultural cold storage system is not just a technical matter; it is a commitment to consumer health and the reputation of Vietnamese agriculture on the global stage.
This article provides a comprehensive and in-depth look at operations at Great Farmer, where advanced technology meets a passion for agriculture.
1. The Importance of Processing and Cold Storage in Agriculture 4.0
Before diving into Great Farmer’s system, it is crucial to understand why this process is vital. According to FAO statistics, post-harvest loss rates in developing countries can reach 20-40%. The primary causes are a lack of processing technology and breaks in the Cold Chain.
A standard factory and cold storage system solve three major problems:
-
Halting Bio-chemical Processes: Produce continues to “breathe” (respire) after harvest. Low temperatures and proper handling slow down ripening and prevent aging.
-
Microbial Control: Eliminating mold and surface bacteria right from the intake stage.
-
Enhancing Commercial Value: Beautiful packaging, standard sizing, and weight accuracy facilitate entry into demanding markets like the US, EU, and Japan.
2. Great Farmer Processing and Packaging Plant: Technology Defines Quality
Great Farmer’s processing plant is designed based on the “One-way Flow” principle to ensure absolute food safety and prevent cross-contamination.
2.1. Multi-Stage Cleaning System
Unlike traditional manual washing methods, Great Farmer applies multi-stage cleaning technology:
-
Ozone Aeration: Removes pesticide residues (if any) and eliminates surface bacteria without damaging the delicate skin of the produce.
-
Ultrasonic Cleaning Technology: Dislodges dirt and debris deep within leaf crevices or rough fruit skins.
2.2. Automated Sorting
We utilize an optical sorting line and weight sensors.
-
Color Sensors: Reject fruits that are under-ripe or have skin blemishes/discoloration.
-
Size/Weight Sensors: Ensure 100% uniformity within each carton. This is critical for export partners and large supermarket chains.
2.3. Modified Atmosphere Packaging (MAP) Technology
In the packaging area, Great Farmer applies Modified Atmosphere Packaging (MAP). This technique alters the air composition inside the packaging, reducing Oxygen and increasing CO2 to levels ideal for each type of produce. This helps the produce “hibernate,” extending shelf-life naturally without the use of chemicals.
3. Great Farmer Cold Storage System: The “Heart” of the Supply Chain.
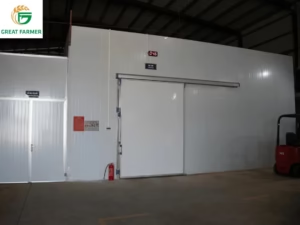
If the processing plant is where produce gets a “makeover,” then Great Farmer’s cold storage is where its freshness is preserved. Our cold storage system is not simply a “giant refrigerator,” but a complex of precision environmental control technology.
3.1. Precision Climate Control
Each type of produce requires a different ideal “temperature zone” and humidity level. Great Farmer’s cold storage is divided into distinct sectors:
-
Medium Temperature Storage (1°C – 15°C): For tropical fruits sensitive to chilling injuries, such as mangoes, bananas, and pomelos.
-
Deep Freeze Storage (IQF): For frozen fruit products.
An IoT (Internet of Things) sensor system monitors the facility 24/7, automatically adjusting temperature deviations to remain within ±0.5°C.
3.2. Pre-cooling Technology
This is the most critical step immediately after harvest. Produce coming from the fields has high “field heat.” If placed directly into cold storage, it will suffer thermal shock and condensation, leading to spoilage. Great Farmer uses Pre-cooling (Forced-air cooling) systems to rapidly lower the core temperature of the product to storage levels, effectively “locking in” freshness instantly.
4. Operational Process: From Farm to Fork
To help partners and customers visualize our meticulous operations, below is a comparison between standard handling and the Great Farmer process.
Comparison Table: Produce Handling Processes
Criteria Traditional Process Great Farmer Process Benefits Harvesting Spontaneous harvesting, left in the sun for long periods. Harvested at technical maturity, immediately moved to shade. Reduces water loss, maintains crispness. Pre-cooling Often skipped. Mandatory. Core temperature lowered within the first 2-4 hours. Prevents early ripening, reduces respiration rate. Cleaning Washed with tap water or wiped dry. Washed with Ozone/Ultrasonic water, air-dried. Removes 99.9% of bacteria, mold, and residues. Sorting Visual sorting, inconsistent. Optical Sorting Machine & Weight Sensors. High uniformity, standardized export codes. Packaging Bulk packing, rudimentary packaging. MAP Standard, impact-resistant packaging, Traceability labels (QR Code). Protects product, ensures information transparency. Storage & Transport Ambient temperature or non-refrigerated trucks. Cold Storage & Dedicated Cold Trucks with temperature monitoring throughout the journey. Ensures “Farm-to-Fork” quality. Expert Note: Strict adherence to the above process allows Great Farmer to reduce spoilage rates to below 5%, whereas the industry average can reach up to 20%.
5. Value Delivered to Partners and Consumers
Investing in a large-scale processing plant and cold storage system is Great Farmer’s long-term commitment to sustainable development. This brings tangible benefits to all stakeholders:
5.1. For Farmers (Raw Material Zones)
-
Solves the “good harvest, bad price” dilemma thanks to the storage and volume regulation capabilities of cold storage.
-
Minimizes post-harvest losses, increasing actual income.
5.2. For B2B Partners (Supermarkets, Exporters)
-
Stable Supply: Thanks to large-capacity cold storage, Great Farmer can supply goods continuously, even during off-seasons.
-
Consistent Quality: Every fruit is identical, facilitating display and inventory management.
-
Meeting International Standards: Processes certified by ISO 22000, HACCP, and GlobalGAP help overcome technical barriers in the EU, US, and Japan.
5.3. For End Consumers
-
Absolute Safety: Clean products inside and out thanks to modern washing and packaging technology.
-
Complete Nutrition: Vitamins and minerals are not lost due to oxidation or high temperatures.
-
Lasting Freshness: Extends preservation time in household refrigerators.
6. Conclusion: Elevating Vietnamese Produce with Tech-Driven Mindsets
At Great Farmer, we don’t just sell agricultural products; we deliver peace of mind. Our modern processing, packaging, and cold storage system is the clearest evidence of our aspiration to elevate the value of Vietnamese agriculture. We believe that only by mastering preservation technology can we confidently bring Vietnamese flavors to the world.
The combination of farmers’ dedication and the precision of high-tech machinery at Great Farmer is the strongest commitment to quality for every product that reaches our customers.
Want to learn more about Great Farmer’s supply solutions?
If you are a partner looking for a high-quality, stable, and export-standard source of agricultural products, or simply a consumer wanting to learn more about our “Clean from the Source” process, please contact us today.
Contact us:
📞 Phone / WhatsApp: +84 785 017 575 | +84 778 078 134 | +84 033 531 3567
📧 Email: mia@greatfarmer.com.vn | clay@greatfarmer.com.vn | loan@greatfarmer.com.vn
🌐 Website: www.greatfarmer.com.vn
 Blog & News